10 Food Processing Equipment Buying Tips for Global Buyers?
Buying food processing equipment across borders is not a simple price comparison. It is a decision about hygiene, capacity, energy, maintenance, and long-term production risk.
Grand View Research estimates that the global food processing equipment market reached approximately USD 52.7 billion in 2023. Its report also projects continued growth through 2030, supported by automation, packaged food demand, and stricter quality expectations. These trends matter to global buyers. A low-cost machine may become expensive when spare parts take eight weeks to arrive.
Food loss adds another practical concern. The FAO’s State of Food and Agriculture report indicates that 13.2% of food is lost between harvest and retail globally. Suitable processing equipment cannot solve every supply-chain weakness, but accurate filling, cooling, drying, and packaging can reduce avoidable waste. Small details matter. A poorly calibrated temperature sensor can damage an entire batch.
PMMI industry reports consistently highlight automation, labor efficiency, and flexible production as major investment drivers. Buyers should therefore examine more than output per hour. Check product-contact materials, cleaning procedures, electrical compatibility, documentation, operator training, and after-sales support. Ask for factory acceptance testing and verified performance data.
The ten buying tips in this guide focus on those practical checks. They are designed for importers, processors, and distributors comparing suppliers across different markets. No checklist removes every uncertainty. Even experienced buyers can overlook installation space or local service capability. That is why quotations, technical drawings, references, and total-cost calculations deserve equal attention. A machine should fit the factory, not merely impress the purchasing team.
Define Your Processing Needs and Production Goals
For global buyers, equipment selection should begin with the product, not the machine. Define the ingredients, product size, moisture range, temperature, shelf-life target, and packaging format. Record actual production data from several batches. One recipe may behave differently during humid or cold seasons. Set measurable goals, such as 1,000 kilograms per hour, 92% yield, or less than 2% product loss. Be realistic.
FAO estimated that 14% of food is lost between harvest and retail worldwide. The UNEP Food Waste Index Report 2024 estimated 1.05 billion tonnes of food waste in 2022. These figures make yield and waste-control targets important when evaluating processing equipment. Ask suppliers to demonstrate performance using your raw materials. Measure output, energy use, cleaning time, changeover losses, and rejected product. A brochure cannot replace a controlled trial.
Production goals should also include labor, utilities, sanitation, maintenance, and future expansion. Check whether local technicians can service critical components. Confirm electrical standards, water quality, compressed-air needs, and spare-part availability before ordering. A line designed only for today’s volume may become restrictive within two years. However, buying excessive capacity can waste capital and increase cleaning losses. This is where planning becomes uncomfortable. Forecasts are never perfect. Leave practical room for growth, but document the assumptions behind every number.
Compare Equipment Types, Features, and Processing Capacity
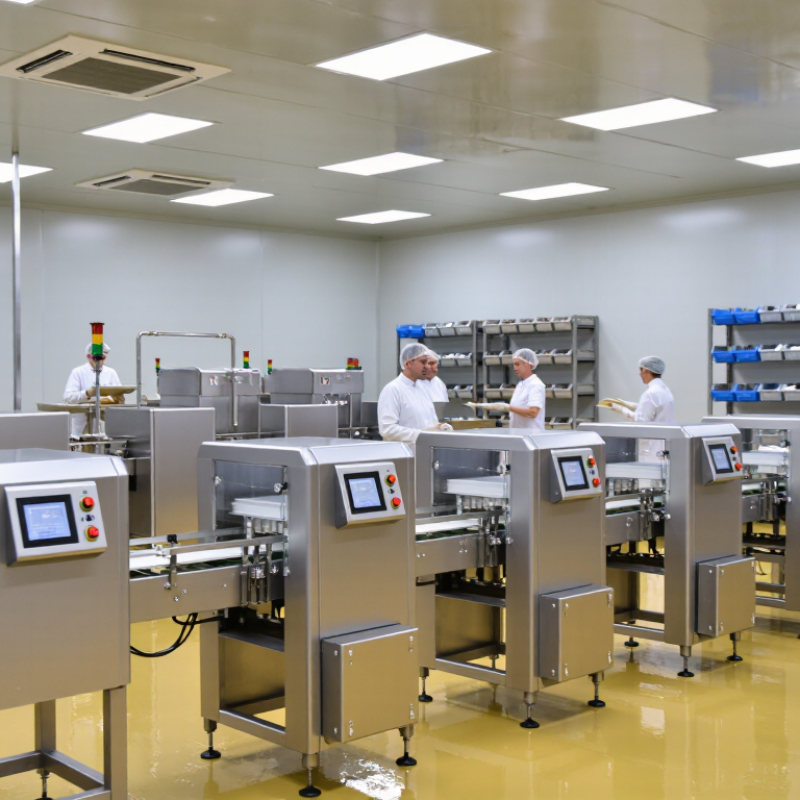
Choosing food processing equipment starts with the product and the job it must do. A batch mixer suits recipes made in measured lots, while a continuous mixer can support steady, high-volume production. A belt dryer moves product through a heated tunnel; a tray dryer offers more control over small batches. The right choice depends on texture, moisture, and how often recipes change. Small details matter. Check whether product-contact surfaces are easy to clean, whether guards are accessible, and whether controls show temperature and speed clearly.
Compare rated capacity with your real production plan. A machine rated for 500 kilograms per hour may deliver less with sticky, fragile, or unevenly sized ingredients. Ask suppliers how capacity was tested, and request a trial using your own product when possible. Measure the feeding, processing, and discharge stages—not just the main machine. Bottlenecks hide there. Also compare power use, changeover time, spare-part availability, and operator training needs. A higher-capacity line is not always better; it may sit idle when demand dips. I would leave room for growth, but not pay for output you cannot use. Specifications help, though they rarely tell the whole story.
Check Materials, Hygiene Standards, and Food Safety Compliance
When buying food processing equipment internationally, inspect every material that touches the product. Food-grade stainless steel, such as 304 or 316, should have clear documentation. Ask for material certificates, surface-finish details, and corrosion-resistance data. Do not rely on the phrase “food safe” alone. Seals, gaskets, hoses, and lubricants also require approval for their intended contact conditions. A shiny surface is not enough.
Hygiene depends on design, not appearance. Check for smooth welds, rounded corners, sloped drainage, and minimal dead spaces. Product residue can hide inside poorly designed joints. Request cleaning instructions and confirm whether the machine supports clean-in-place procedures. If manual cleaning is required, inspect how quickly operators can remove guards, screens, and product-contact parts. Small gaps matter. They can increase cleaning time and contamination risk.
Food safety compliance requires evidence that can be reviewed. Ask for current certificates, test reports, risk assessments, and traceability records. Confirm which standards apply in the installation country, because requirements can differ across markets. Review factory acceptance tests and installation checks before shipment. A supplier may provide complete paperwork, but missing maintenance records can still create problems later. This is where buyers often underestimate responsibility. Equipment should be evaluated with the actual ingredients, cleaning chemicals, temperatures, and production volume in mind. The factory floor may reveal issues that a catalog never shows.
Plan Installation, Maintenance, Training, and After-Sales Support
For global buyers, an equipment purchase is also an installation and service plan. Before shipment, confirm floor loading, doorway clearance, utility connections, drainage, and local voltage requirements. Ask the supplier for layout drawings and a commissioning checklist. A crate arriving before the site is ready can sit idle while production plans change.
Maintenance needs should be clear before the first production run. Request recommended spare-parts lists, service intervals, and plain-language troubleshooting steps. FAO’s 2019 State of Food and Agriculture estimated that 14% of food is lost between post-harvest and retail. Reliable equipment cannot prevent every loss, but prompt maintenance can help limit avoidable stoppages and product waste. Small details matter. Confirm which parts are stocked nearby and how quickly remote technical support can respond.
Training deserves its own schedule, not a brief handover at the machine. Deloitte and The Manufacturing Institute projected in their 2024 report that 1.9 million U.S. manufacturing jobs could go unfilled by 2033. Buyers should plan for operator and technician training, with translated materials and practical sessions on cleaning, changeovers, and fault recovery. Ask who provides refresher training after staff turnover. The plan may still miss something; production conditions rarely match a demonstration exactly. That is why acceptance testing should use the buyer’s actual product, packaging, and operating shift.
10 Food Processing Equipment Buying Tips for Global Buyers
Plan installation, maintenance, training, and after-sales support before selecting equipment.
Each bar counts practical buyer checks in this planning framework, not survey results. Use the chart to identify topics to confirm with suppliers; installation requirements, maintenance intervals, training needs, and support coverage vary by equipment and site.